


₹ 33500
• Delivery will be made after the payment is credited to our bank account.
• Transportation charges are extra and will be charged on an actual basis.
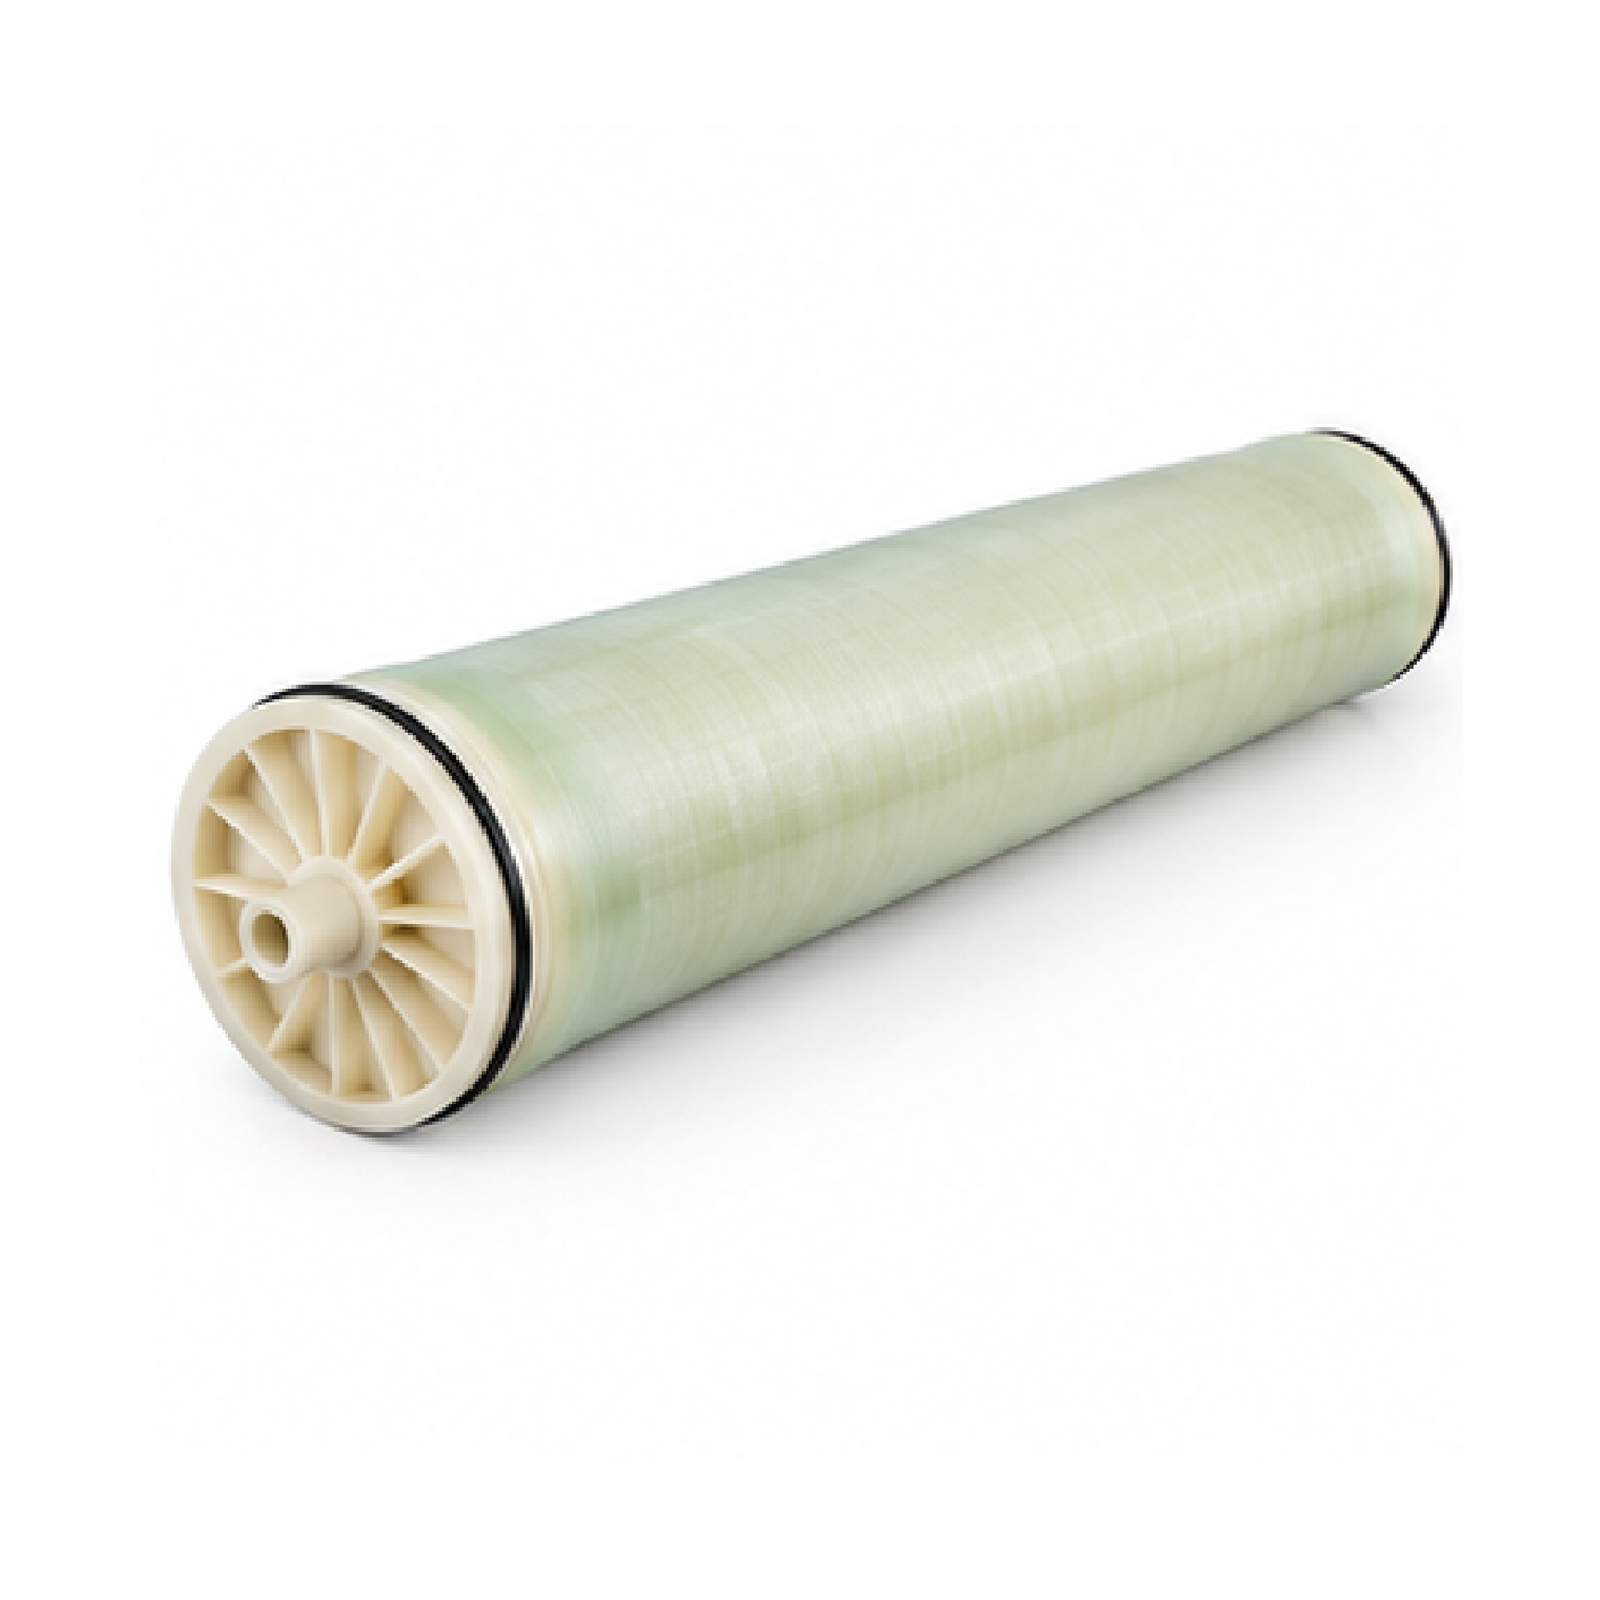
The Veolia AG 8040 FM RO Membrane is a high-performance industrial brackish water reverse osmosis membrane designed for efficient water purification. Featuring advanced Thin-Film Membrane (TFM) technology and fiberglass outer wrapping, it delivers excellent salt rejection and reliable permeate flow. Ideal for industrial RO plants, mineral water plants, commercial water treatment systems and large-scale water purification applications.
The Veolia AG 8040 FM RO Membrane is an industrial reverse osmosis membrane designed for brackish water purification applications. It belongs to the Veolia AG Series, known for high water flux and effective sodium chloride rejection.
Manufactured using proprietary A-Series Thin-Film Membrane (TFM) technology, this membrane helps remove dissolved salts and impurities from feed water to produce high-quality purified water.
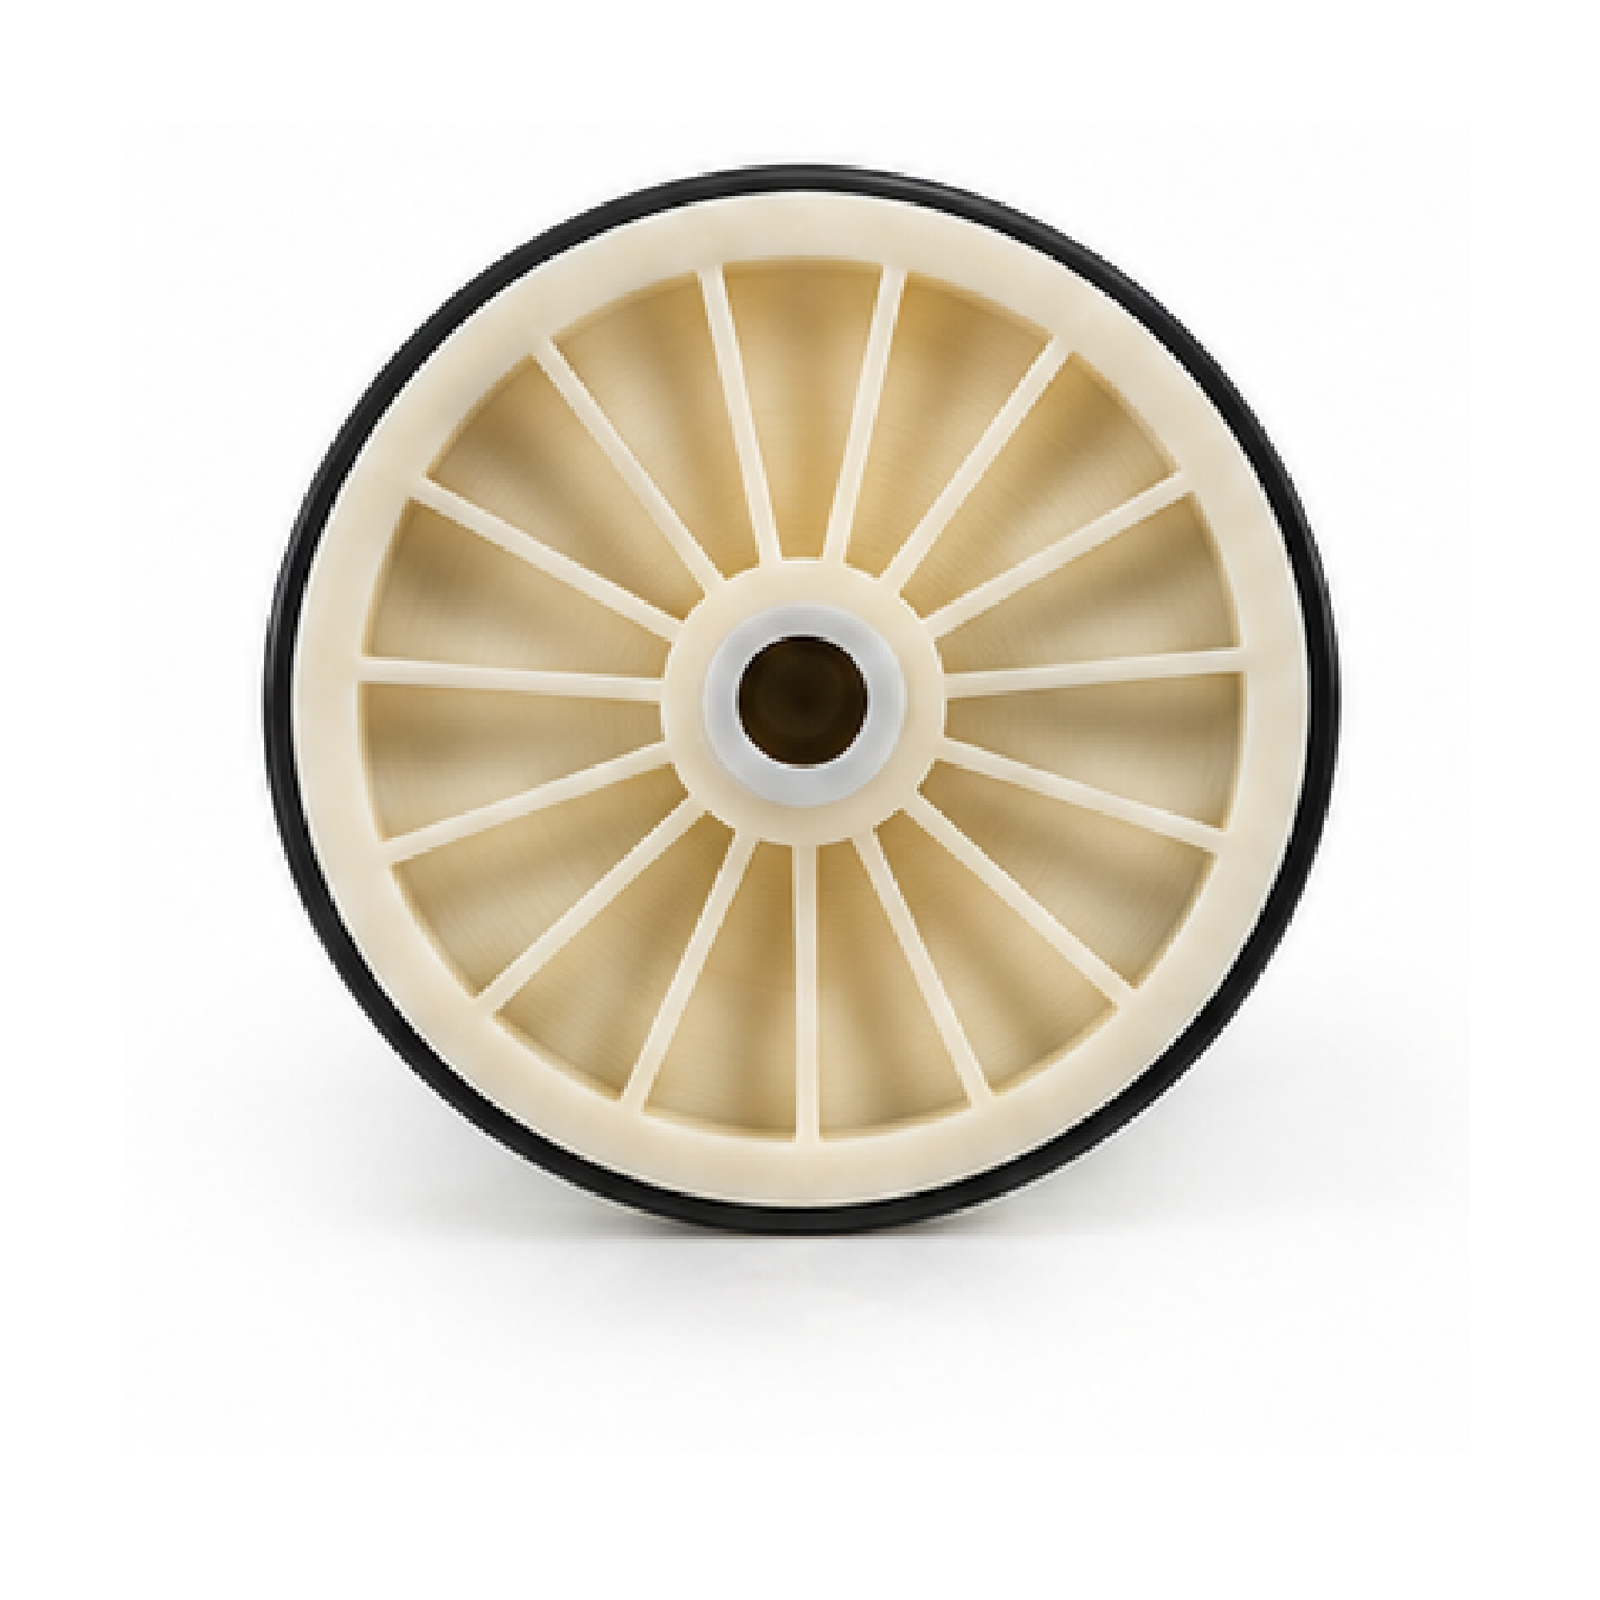
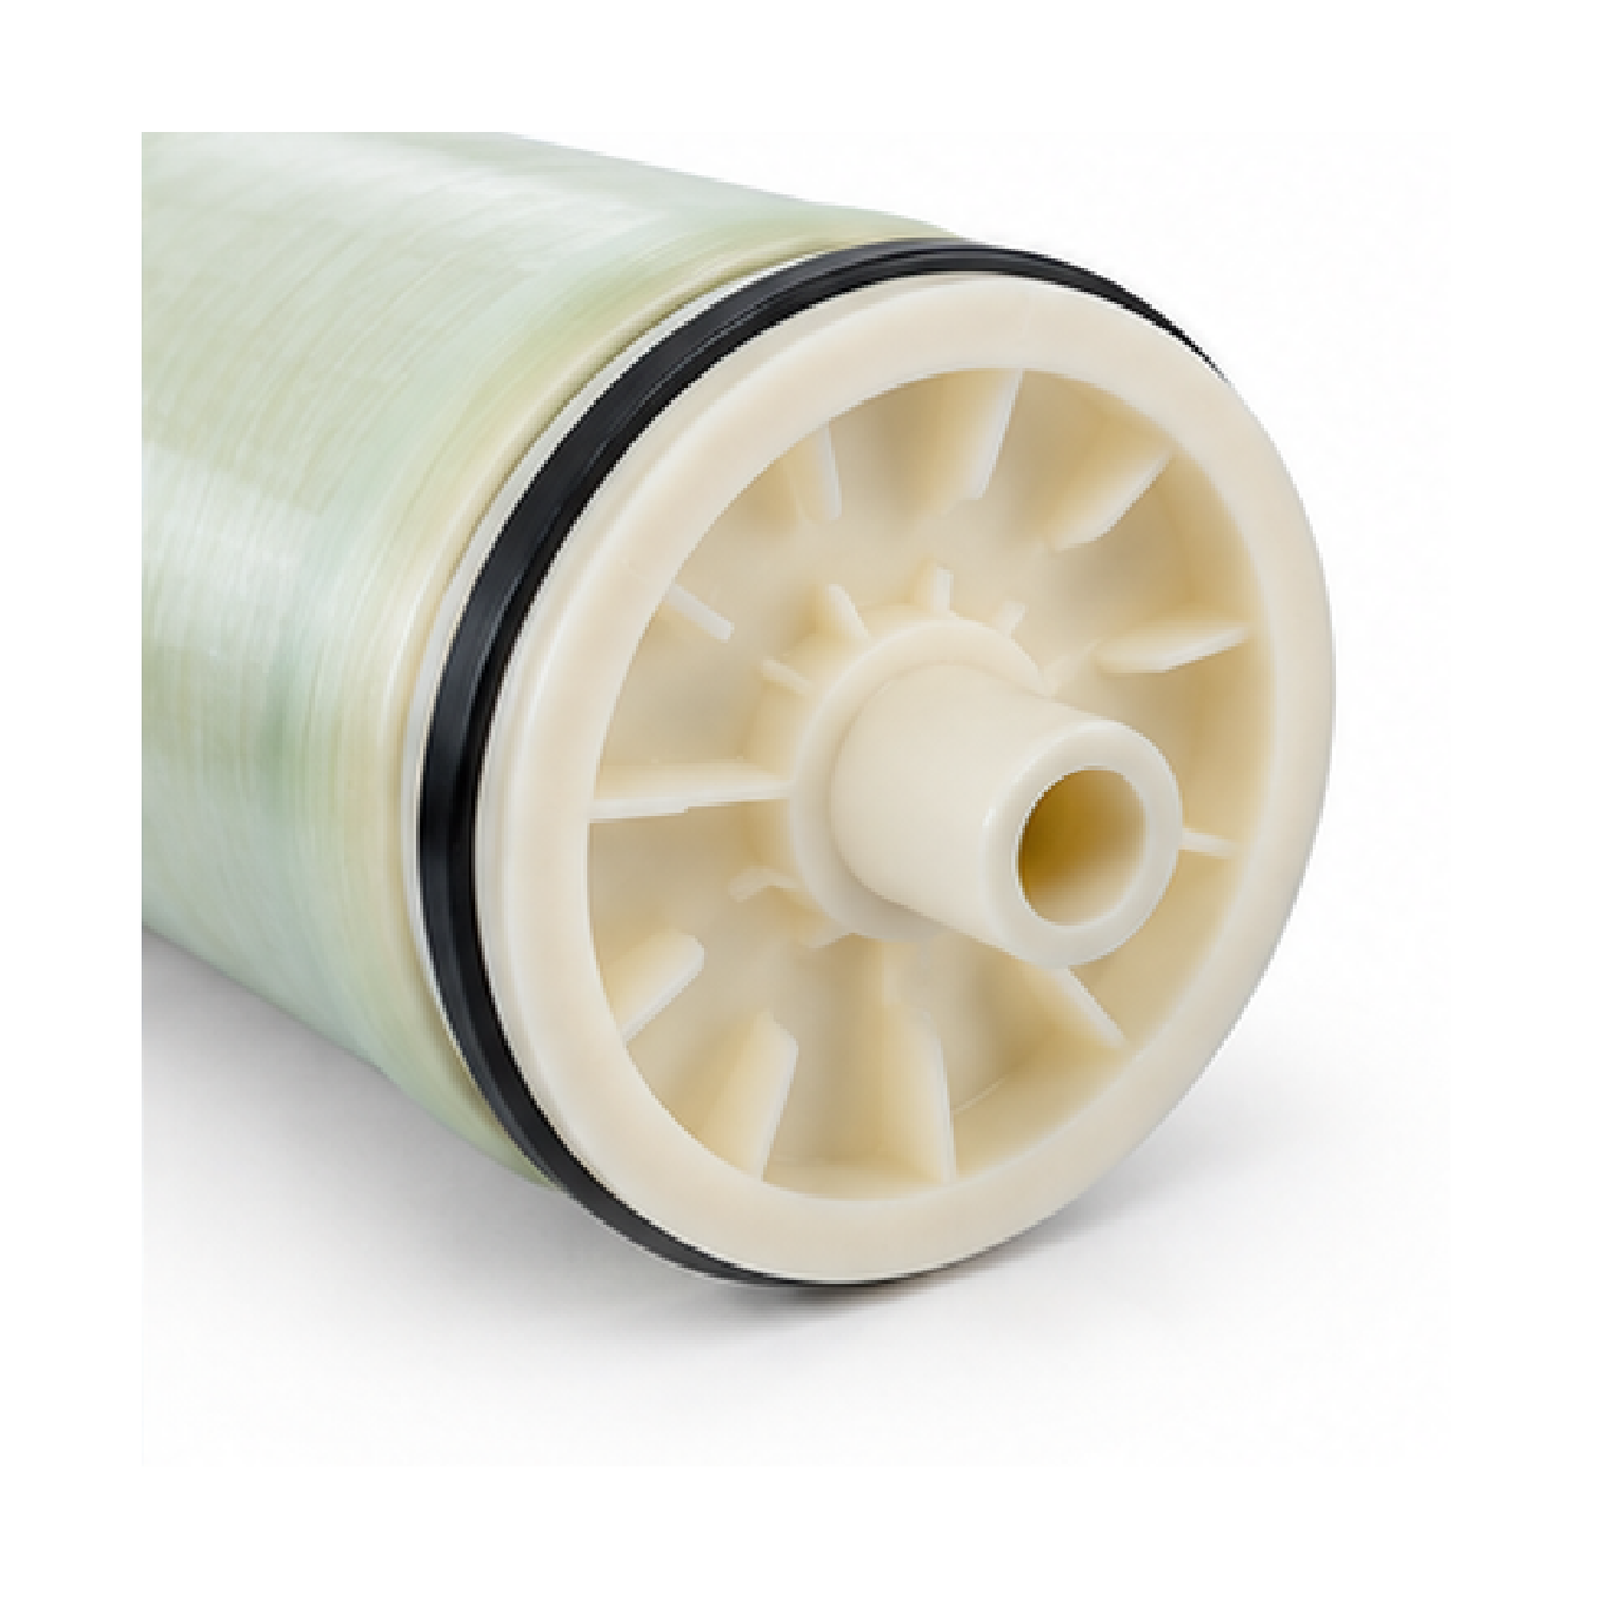
The AG8040FM features an 8-inch × 40-inch configuration with fiberglass outer wrapping, making it suitable for industrial RO pressure vessels. Its high salt rejection and dependable water flow make it an excellent choice for industrial water treatment, mineral water manufacturing and commercial RO systems.
Advanced TFM membrane technology.
High salt rejection performance.
365 sq. ft. active membrane area.
Fiberglass outer wrapping.
Spiral-wound membrane construction.
High permeate flow capacity.
Efficient brackish water purification.
Designed for industrial RO systems.
| Parameter | Specification |
|---|---|
| Brand | Veolia |
| Product Series | AG Series |
| Model Reference | AG8040F |
| Membrane Type | Brackish Water RO Membrane |
| Membrane Size | 8040 (8″ × 40″) |
| Membrane Technology | A-Series Thin-Film Membrane (TFM) |
| Construction | Spiral Wound |
| Outer Wrap | Fiberglass |
| Active Membrane Area | 365 sq. ft. (33.9 m²) |
| Average Permeate Flow | 10,000 GPD (37.9 m³/day) |
| Average Salt Rejection | 99.5% |
| Minimum Salt Rejection | 99.0% |
| Typical Operating Pressure | 200–225 PSI |
| Maximum Operating Pressure | 600 PSI |
| Maximum Operating Temperature | 50°C |
| Continuous Operating pH | 2–11 |
| Cleaning pH Range | 1–13 |
| Maximum Feed Water SDI | 5 |
| Maximum Feed Water Turbidity | 1 NTU |
Industrial RO Water Treatment Plants
Mineral Water Manufacturing Plants
Packaged Drinking Water Plants
Commercial RO Systems
Pharmaceutical Industries
Food and Beverage Industries
Industrial Process Water Treatment
Brackish Water Purification Systems
Manufacturing Industries
Produces high-quality purified water.
Reduces dissolved salts and impurities.
Supports efficient water purification.
Helps maintain consistent water quality.
Suitable for large-capacity RO plants.
Reliable industrial water treatment performance.

Get Best Price Quotation